Machine Downtime Tracking
That Shows the Cost.
Most shops know a machine went down. Few can say why, or what it cost the order.
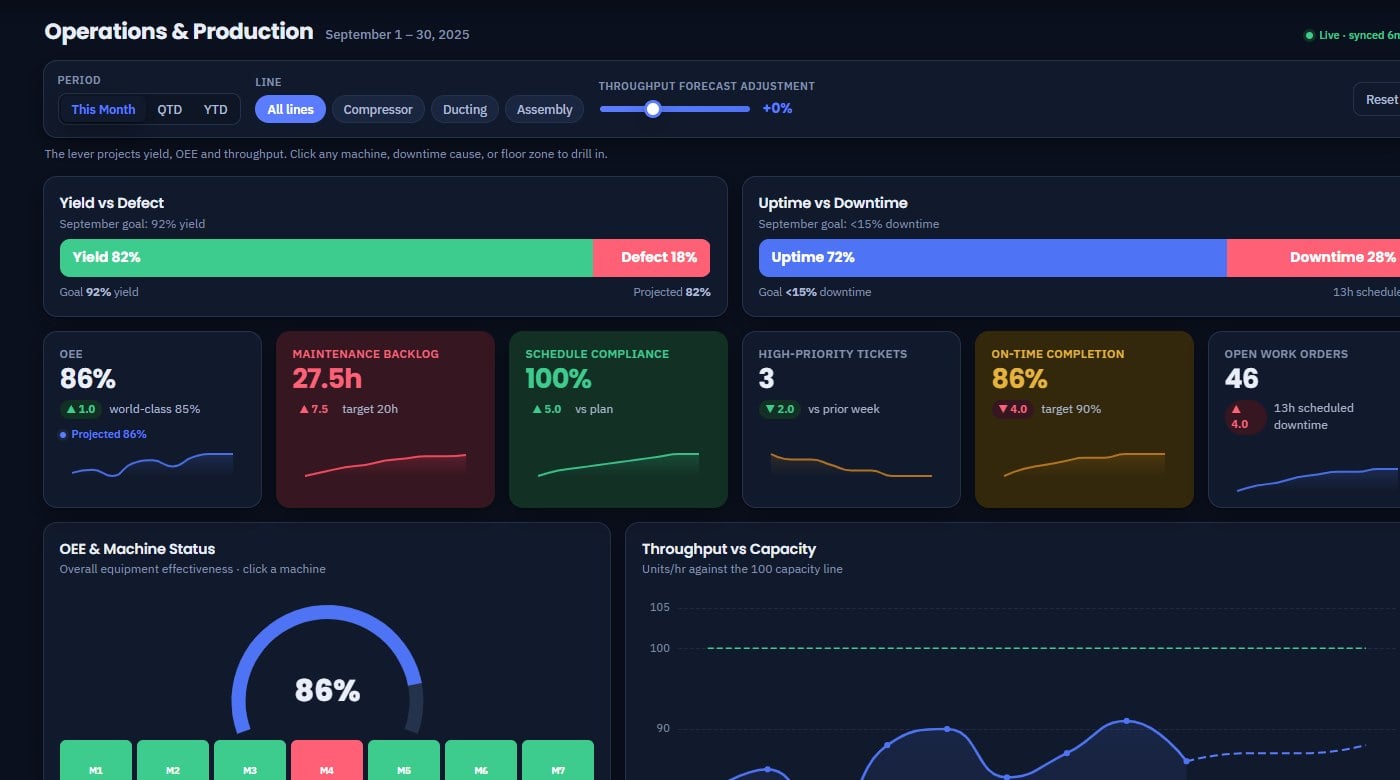
We connect machine signals to your ERP so every stop gets a reason, a length and a cost.
Every stop has a price.
Most shops never see it.
RADIN helps mid-market manufacturers build and protect their investment in AI with an independent AI readiness assessment before any deal is signed, an optional fractional Chief AI Officer, and the ERP and CRM systems to match, with no software quota behind the advice.
• HEAR IT FROM A CLIENT
See what our clients say
“RADIN stepped in and salvaged a very significant go-live date in two or three months, when we were at a failure point. That was massive for us as an organization. You said, listen, we can do this, and you’ve been able to do that.”
Rick Pace
HME. Three years working with RADIN.
Why downtime stays invisible
Six ways stoppages hide in a shop, and what changes when they’re tracked.
Stops go on a whiteboard. Every stop is captured the moment the machine goes idle.
Nobody knows why it stopped. Operators pick a reason in two taps while it’s fresh.
The late order has no cause. Each stop is tied to the job it held up.
Maintenance runs on the calendar. Service happens when the machine’s data calls for it.
The veteran hears it first. Drift gets flagged before it turns into a breakdown.
OEE is a guess. Availability comes from real stops, not memory.
Start with the one machine that hurts most when it stops.
Get the reason codes right there, then add the next one.
• THE GUIDE, BY PARKER HENDRICKS
Written by Parker Hendricks, VP of Sales at RADIN Dynamics. Parker grew up on the floor of his father’s metal fabrication shop in Monroe, Georgia, and holds the AI seat at the Georgia Manufacturing Alliance. Updated September 2026.
Our view: start with the one machine that hurts most when it stops. A plant-wide rollout before anyone trusts the reason codes is money sitting on a shelf.
Why nobody can say what a stoppage cost
Ask most plant managers how much downtime cost last month and you’ll get a shrug or a guess. The stop happened, someone restarted the machine, and by the end of the shift a long stop became “a few minutes” on the whiteboard. Nobody tied it to the order that shipped late or the overtime it caused.
At the big end of the market, the numbers are huge. Siemens estimates unplanned downtime now costs the world’s 500 largest companies about 11% of their revenue, and an hour down in an automotive plant runs about $2.3 million (Siemens, The True Cost of Downtime 2024). Your shop isn’t a car plant, but the math works the same way at your scale: lost hours, late orders and overtime, on the machines you can least afford to lose.
Three ways plants track downtime
| Method | What it costs | What you actually learn | Where it breaks |
|---|---|---|---|
| Paper log or whiteboard | Almost nothing up front | That a stop happened, roughly | Short stops never get written down, and nobody adds it up |
| Spreadsheet | Someone’s time every shift | Totals by machine, if it’s kept up | The person who maintains it leaves or gets busy |
| Connected monitoring | Sensors or controller connections plus software | Every stop, its length, its reason and its cost by job | Reason codes nobody agreed on |
The knowledge walking out the door
About one in four US manufacturing workers is 55 or older (BLS Current Population Survey, 2025). In a lot of shops, the real downtime tracking system is the veteran who can hear a spindle going bad from across the floor. Deloitte and The Manufacturing Institute estimate manufacturers could need as many as 3.8 million new workers by 2033, and that 1.9 million of those jobs could go unfilled (Deloitte and The Manufacturing Institute, 2024). When that veteran retires, what they knew should already be in the system.
What good tracking feeds later
Once stops are captured honestly, the numbers start working for you. OEE, the measure of availability, performance and quality, stops being a guess. The widely used benchmark for world-class OEE is 85%, and plenty of plants run well below it. Maintenance can move from the calendar to the machine’s actual condition. And later, when you want AI to predict failures or schedule around them, it has years of trustworthy history to learn from.
How to start
- Pick the one or two machines where a stop hurts most.
- Agree on a short list of reason codes with the operators who’ll use them.
- Connect those machines and send each stop into your ERP against the job.
- Review the numbers weekly for a month before adding more machines.
Where to start. Book a 30 minute call. Bring the workflow you want to fix, or the proposal someone just sent you. Your AI readiness assessment is included, and if your shop isn’t ready for AI yet, you’ll hear it from us first. Book a 30 minute call.
Track it honestly.
Then fix what it shows.
Most older machines can be monitored with add-on sensors or by reading the controller, so you keep the equipment you have. The stop data flows into your ERP against the job, where planning and maintenance can act on it.
Start where your shop is
A broken system needs the foundation first. Decent systems with no AI plan need the judgment. Most shops need both, in that order.
-
AI readiness assessment
Included when you work with us. Where AI fits on your floor and where it doesn't, before a dollar is spent. -
Fractional Chief AI Officer
$5,000 a month, 90 days then month to month. 16 hours, tracked. Any vendor quote answered inside 48 hours. -
CRM Health Check
Free. A current-state map, a 90-day plan and a one-pager for the board. Shops from $10M and 20 people. -
ERP for manufacturers
From $10M to $300M, with our own tool for the move off QuickBooks or a legacy system. -
CRM for manufacturers
Quoting and the customer file, connected to the floor and the books. Built only for manufacturers.
The numbers behind this
Siemens puts unplanned downtime at 11% of revenue for the world’s 500 largest companies (2024). One in four US manufacturing workers is 55 or older (BLS, 2025).
Zero
software quota behind our advice
Questions
Machine Downtime Tracking: Common Questions
What is machine downtime tracking?
It’s recording every time a machine stops, for how long and why, then tying that stop to the job, the order and the cost.
What are the ways to track machine downtime?
Paper logs, spreadsheets and connected machine monitoring. Paper is cheap and usually incomplete. Spreadsheets help until nobody updates them. Connected monitoring captures the stop on its own and asks the operator only for the reason.
Do we have to replace our machines?
No. Most older machines can be monitored with add-on sensors or by reading the controller, so you keep the equipment you have.
Is this only for large plants?
No. We work with manufacturers from 20 to 1,000 people, and a small shop feels an unplanned stop on its biggest machine faster than anyone.
What should we fix before buying a monitoring system?
Agree on your downtime reason codes and who owns them. Software can’t fix a list of reasons nobody uses.
• Built only for manufacturers
We know which floors
we belong on
Manufacturing of every kind, from job shops and fabricators to machinery builders and the suppliers feeding aerospace, defense, medical and electronics.
Who we work with
Manufacturers with 20 to 1,000 people and $10M+ in revenue, from founder-led job shops to larger manufacturing organizations. If aging or disconnected systems are holding you back, we help you plan and deliver the right AI, ERP, and CRM improvements.
Manufacturing
Know what a job really cost. See the floor without three phone calls.
People who have stood
where you stand
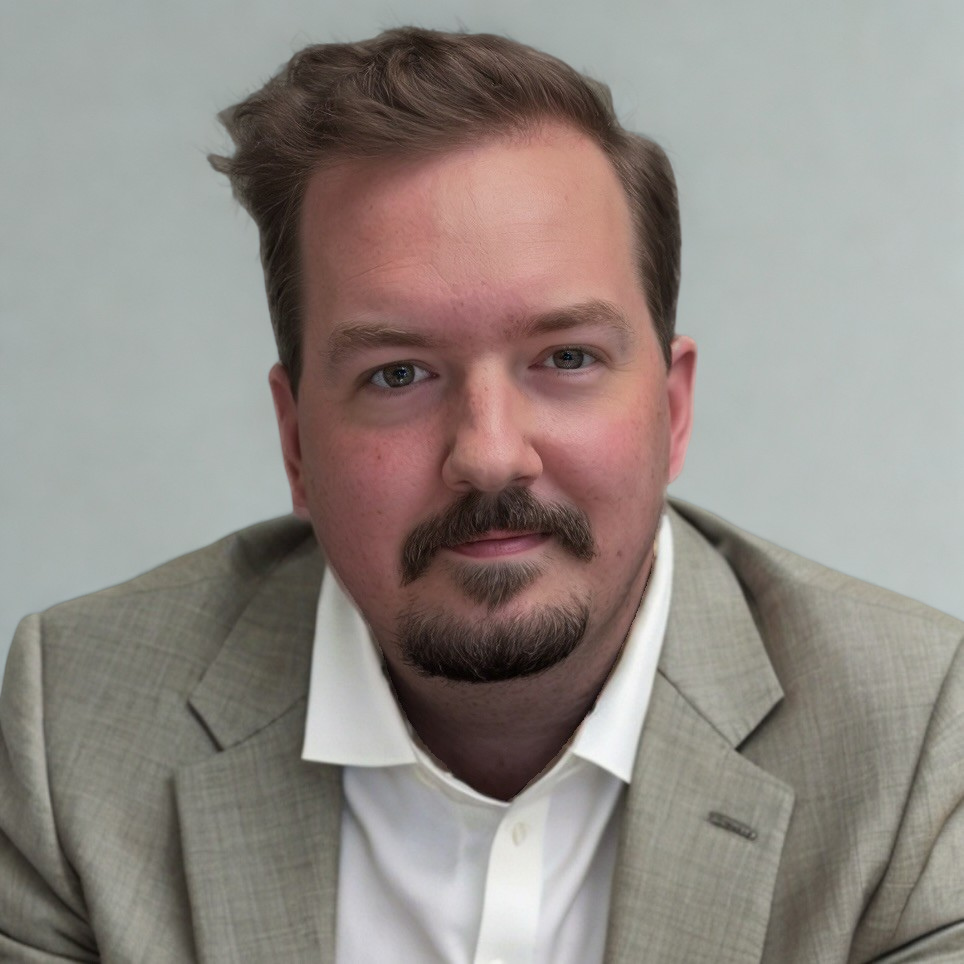
Parker Hendricks grew up on the floor of his father’s metal fabrication shop in Monroe, Georgia. He holds the AI seat at the Georgia Manufacturing Alliance and hosts The unManufactured Show.
Sixteen years of Dynamics delivery behind him, a hybrid US and offshore team, and one rule: we show up, we do what we say, and we don’t disappear after the handshake.
“We build on the Microsoft stack, and where it fits your shop we will scope it. So here is our rule: we disclose what we earn on anything we recommend.”
Parker Hendricks, VP of Sales
People who have stood
where you stand
Parker Hendricks grew up on the floor of his father’s metal fabrication shop in Monroe, Georgia. He holds the AI seat at the Georgia Manufacturing Alliance and hosts The unManufactured Show.
Sixteen years of Dynamics delivery behind him, a hybrid US and offshore team, and one rule: we show up, we do what we say, and we don’t disappear after the handshake.
“We build on the Microsoft stack, and where it fits your shop we will scope it. So here is our rule: we disclose what we earn on anything we recommend.”
Parker Hendricks, VP of Sales
Book a 30 minute call
Bring the machine that stops more than it should. We’ll show you what tracking it would take, and what the data could tell you in the first month.